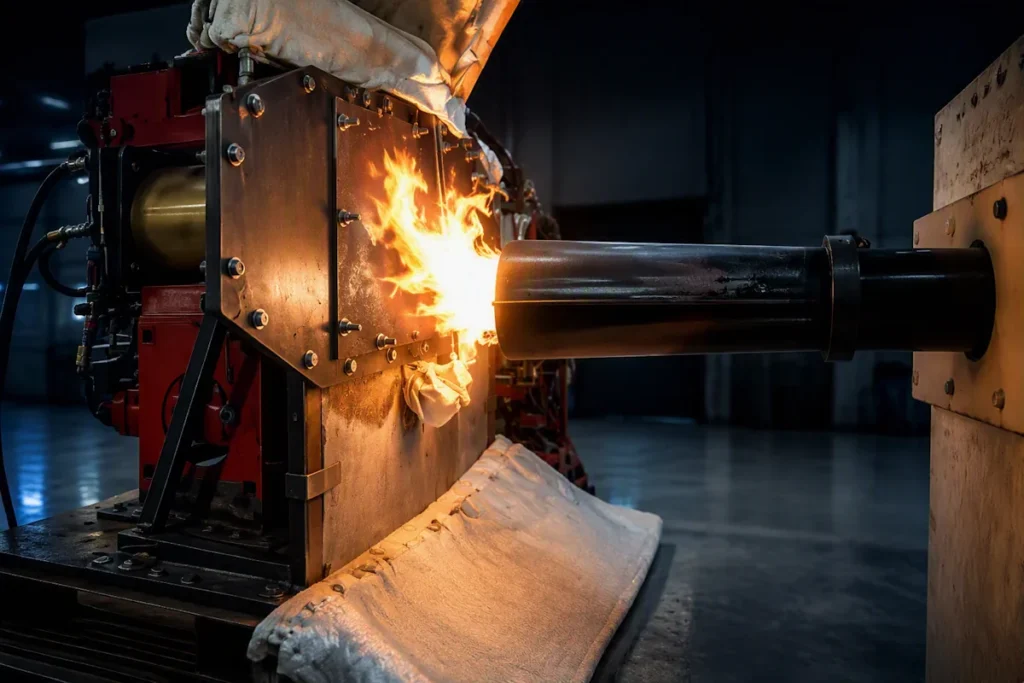
FAA Powerplant Engineering Report No. 3A defines a standard fire-test apparatus and procedure originally developed to determine the fire resistance of flexible aircraft hose assemblies. Revised in March 1978, the report describes a test environment combining a controlled oil-burner flame, fluid flow, pressure, temperature, vibration and airflow.
The original reference burner was a modified Lennox OB-32. When that burner became commercially unavailable, the FAA characterised its flame and used the resulting performance data to evaluate alternative modified burners. These included the Carlin 200 CRD, Stewart-Warner HPR-250 and Stewart-Warner FR-600.
The report therefore establishes two related but different activities:
Burner-configuration qualification, which demonstrates that a burner design and modification state can reproduce the required flame characteristics.
Operational burner standardisation, which confirms that the burner achieves the required temperature and heat-transfer performance before it is used for a fire test.
This distinction matters. Possession of a listed burner model does not demonstrate that the actual burner is correctly modified, maintained or adjusted. Equally, a burner that achieves one parameter but fails another has not reproduced the complete Report 3A fire environment.
Within an aerospace or space verification programme, burner control forms part of the wider test-equipment assurance process. The resulting fire-test evidence is only defensible when the burner configuration, instrumentation, operating settings, calibration data and test geometry are controlled and traceable.
FAA 3A burner qualification is the process used to demonstrate that a defined modified burner configuration produces flame characteristics equivalent to those established by FAA Powerplant Engineering Report No. 3A.
Operational verification, often described in the report as standardisation, confirms that the qualified or accepted burner produces the required test flame under the settings and conditions used for a particular test campaign.
The engineering objectives are to demonstrate:
A controlled flame-temperature profile.
Adequate flame width and coverage.
A defined heat-transfer rate to the standard copper-tube device.
A controlled thermal-energy output.
Stable combustion.
Repeatable fuel and airflow settings.
Reproducible burner-to-specimen geometry.
Traceable evidence supporting the validity of the fire test.
Report 3A does not:
Certify every burner of a listed commercial model.
Approve an unmodified commercial heating burner.
Replace the applicable aircraft or engine regulations.
Define every modern powerplant fire-test application.
Replace ISO 2685, FAA AC 20-135A or SAE AS6826.
Make the test laboratory the certification authority.
Guarantee that a component test will be accepted.
| Activity | Purpose | Typical trigger |
|---|---|---|
| Burner-configuration qualification | Demonstrate that a burner design and modification state can reproduce the required Report 3A flame characteristics. | New burner type, new modification or equivalency study. |
| Initial commissioning | Confirm the installed burner, fuel system, airflow system, instrumentation and controls function together correctly. | New equipment or major facility change. |
| Pre-test standardisation | Adjust and verify the flame before fire-test exposure. | Before an applicable fire test. |
| Post-maintenance verification | Confirm that maintenance has not changed burner performance. | Nozzle, cone, deflector, pump, motor or airflow-system change. |
| Periodic verification | Detect drift, deterioration or configuration change. | Laboratory quality-system interval. |
| Post-test validation | Confirm continued burner performance where the governing test method requires it. | Defined by the applicable procedure or customer specification. |
The applicable test method must be checked carefully. Report 3A, ISO 2685, customer procedures and SAE AS6826 do not use identical calibration and post-test validation rules.
Identify applicable fire-resistance requirements.
Determine whether the hardware is installed within or adjacent to a designated fire zone.
Define the required fire-intended functions.
Select the governing fire-test method.
Identify critical flame-impingement locations.
Produce representative qualification hardware.
Control materials, seals, joints, fittings and interfaces.
Record the test-article configuration.
Confirm conformity where required.
Prepare the test fixture.
Install instrumentation.
Configure pressure, flow, temperature, airflow and vibration.
Verify burner and fixture geometry.
Complete safety and readiness reviews.
Standardise the burner.
Conduct the fire-resistance test.
Monitor the required functions and boundary conditions.
Record the fire exposure and test-article response.
Review deviations and anomalies.
Confirm burner and instrumentation traceability.
Link test data to the approved procedure.
Close deviations.
Complete the fire-test report.
Update the verification or certification compliance matrix.
An uncontrolled burner can expose a test article to the wrong thermal environment.
An under-severe flame can create a false pass. An excessively severe or poorly distributed flame can create an unrepresentative failure. Both outcomes can lead to redesign, repeat testing, certification challenge or unsafe engineering conclusions.
FAA Report 3A has historically supported flexible-hose fire testing and is referenced through wider aircraft fire-test guidance, standards and customer specifications.
Its applicability must be established through the governing test requirement. The report should not be cited as a universal compliance route for every aircraft component.
Measured evidence is generated through:
Flame-temperature assessment.
Temperature-profile mapping.
Copper-tube heat-transfer measurement.
Thermal-energy assessment.
Fuel-flow control.
Air-pressure control.
Burner-configuration inspection.
Test-distance verification.
Instrumentation traceability.
A test article cannot be meaningfully assessed unless the applied exposure is known.
The evidence chain is:
Controlled burner configuration → valid standardisation → controlled test geometry → valid exposure → defensible test result
Reliable fire testing supports assurance that safety-critical hardware can maintain its required function or containment performance during the defined fire exposure.
For space programmes, this may be relevant to launch-vehicle propulsion systems, ground-support systems, test facilities or other applications where the customer invokes an aircraft-derived fire-test method. The applicability must be established by the programme.
FAA Report 3A established controlling characteristics using the modified Lennox OB-32 as the reference burner.
Temperature measurements through the horizontal centreline should indicate:
2,000°F ±150°F
Across a horizontal distance of at least seven inches
Using the specified temperature-measurement arrangement
This is a flame-profile requirement, not a single centre-point reading.
The total heat transfer to the half-inch copper tube should be:
Not less than 4,500 Btu/h
Not greater than 4,650 Btu/h
The main body of the report also identifies 4,500 Btu/h as the minimum standardisation value required for the test flame.
Report 3A separately describes total thermal energy in Btu/ft²/s using the calorimeter method and the tolerance notation contained within Appendix III.
This parameter should not be casually treated as interchangeable with the 4,500 Btu/h copper-tube heat-transfer result. The measurement method, exposed area and governing acceptance logic must be stated.
The accepted modified burners were configured to produce a diffused flame approximately:
Six inches vertically
Eleven inches horizontally
The objective was a homogeneous temperature gradient across the area used to expose the hose fitting and adjacent hose.
The modified Lennox OB-32 was the original reference configuration. It became unavailable commercially, which led to the FAA evaluation of alternative burners.
The report records reference performance of:
Heat transfer: approximately 4,574 Btu/h
Thermal energy: approximately 9.8 to 10.8 Btu/ft²/s
Flame oxygen concentration: approximately 5% to 11%
The Carlin 200 CRD was modified to reproduce the reference flame.
The documented modifications included:
An 80-degree fuel nozzle rated at 2.25 gal/h.
Fuel delivery adjusted to approximately 2.04 gal/h at 97 psig.
Removal of retention and throttle rings and associated forward components.
Installation of a perforated support disc.
Reduction of the air-tube diameter.
Installation of stainless-steel fuel deflectors.
Installation of a static-pressure port.
Addition of the specified burner extension.
Adjustment of air-tube pressure.
The report records a heat-transfer result of approximately 4,545 Btu/h and total thermal energy of approximately 9.3 to 11.2 Btu/ft²/s for the evaluated Carlin configuration.
The evaluated HPR-250 configuration used a revised nozzle, reducing cone, deflectors, pressure port and extension tube.
The report records:
Heat transfer: approximately 4,646 Btu/h
Thermal energy: approximately 9.3 to 10.1 Btu/ft²/s
The evaluated FR-600 configuration also used a defined nozzle, reducing cone, deflectors and extension tube.
The report records:
Heat transfer: approximately 4,466 Btu/h
Thermal energy: approximately 9.9 to 10.9 Btu/ft²/s
The recorded heat-transfer value is below the 4,500 Btu/h minimum stated elsewhere in the report. This internal inconsistency is one reason engineers should not rely on a model name or summary table without reviewing the full applicable requirement and current customer acceptance basis.
The standardisation apparatus measures the rate at which the flame transfers heat to a water-cooled copper tube shaped to represent the hose region exposed during testing.
The apparatus includes:
A constant-head water supply.
A metering valve.
A half-inch copper heat-transfer tube.
Inlet and outlet temperature sensors.
A measuring container or weighing arrangement.
A controlled tailpipe drop.
Mixing material within the measuring assembly.
Heat-deflector shields.
A controlled burner-to-tube position.
Report 3A specifies:
Water inlet temperature between 50°F and 70°F.
Water flow of 500 lb/h.
Approximately one US gallon per minute.
Cleaning of the external copper-tube surface before each test.
The burner is adjusted to produce:
A flame of 2,000°F ±150°F.
Measured four inches beyond the burner extension.
A standardised heat transfer of at least 4,500 Btu/h.
The burner is allowed to stabilise for three minutes.
The warm-up should occur away from the heat-transfer tube to minimise carbon build-up on the copper surface.
After stabilisation:
The burner is positioned against the standardisation device.
Inlet and outlet water temperatures are recorded every 30 seconds.
Recording continues for three minutes.
The average inlet-to-outlet water-temperature difference is calculated.
The average temperature difference is multiplied by the 500 lb/h water-flow rate.
Heat transfer, Btu/h = average water-temperature rise, °F × water-flow rate, lb/h
At a water-flow rate of 500 lb/h, a 9°F average rise corresponds to:
9°F × 500 lb/h = 4,500 Btu/h
FAA Report 3A is not an ECSS standard. ECSS does not automatically require this burner or procedure.
Where a space project invokes FAA Report 3A, ISO 2685, SAE AS6826 or a customer-derived method, the activity may sit within the programme’s controlled verification system.
Potentially relevant ECSS standards include:
ECSS-E-ST-10, System Engineering General Requirements.
ECSS-E-ST-10-02, Verification.
ECSS-E-ST-10-03, Testing.
ECSS-Q-ST-20, Quality Assurance.
Their applicability must be confirmed through project tailoring.
A space programme may require:
Verification requirement allocation.
Defined verification methods.
Test-level and model-level justification.
Controlled test specifications.
Test readiness review.
Equipment suitability evidence.
Measurement traceability.
Uncertainty assessment.
Configuration control.
Non-conformance control.
Verification close-out evidence.
Prime contractors, launch-system integrators and agencies may impose controls beyond Report 3A, including:
Wider flame mapping.
Additional repeat runs.
Extended operating envelopes.
Alternative burner orientations.
Independent witnessing.
Additional calibration intervals.
Formal uncertainty budgets.
Configuration audits.
Facility qualification.
Software and data-acquisition validation.
Post-test validation requirements.
Define whether the activity is design qualification, commissioning or routine standardisation.
Identify the governing standard and revision.
Review the burner configuration.
Define the intended test application.
Establish acceptance criteria.
Define the instrumentation.
Define uncertainty and traceability requirements.
Establish witness and reporting requirements.
Record burner make, model and serial number.
Record the complete modification state.
Inspect the nozzle, air tube and reducing cone.
Inspect deflectors and support hardware.
Inspect the extension tube.
Verify fuel type and supply condition.
Verify fuel pressure and flow controls.
Verify airflow and static-pressure measurement.
Confirm instrument calibration status.
Clean the copper tube.
Verify apparatus geometry.
Complete the safety assessment.
Ignite the burner.
Establish stable combustion.
Set the defined fuel and air conditions.
Complete the horizontal temperature-profile map.
Complete copper-tube heat-transfer measurement.
Complete any required thermal-energy assessment.
Repeat runs where required.
Record environmental and operating conditions.
Record burner behaviour and visible instability.
Compare each result with the applicable limits.
Review temperature uniformity.
Review heat-transfer repeatability.
Review thermal-energy results.
Assess run-to-run variability.
Examine fuel and airflow stability.
Review instrument uncertainty.
Review deviations.
Confirm whether the data support the stated qualification objective.
Issue the qualification or verification report.
Record the approved configuration.
Record operating settings and permitted tolerances.
Define maintenance controls.
Define periodic-verification intervals.
Archive raw data and certificates.
Close non-conformances.
Release the burner for the defined scope of testing.
Check:
Burner model.
Fuel nozzle specification.
Fuel-delivery rate.
Fuel pressure.
Air-tube diameter.
Reducing-cone geometry.
Deflector quantity, position and dimensions.
Support-disc configuration.
Extension-tube geometry.
Static-pressure-port location.
Motor and blower configuration.
Fuel-pump configuration.
Assess:
Horizontal centreline.
Required seven-inch hot region.
Individual temperature measurements.
Average temperature.
Uniformity.
Edge fall-off.
Repeatability.
Instrument condition.
Sensor response.
Control:
Copper-tube dimensions.
Tube cleanliness.
Water temperature.
Water flow.
Burner position.
Warm-up period.
Measurement duration.
Sampling interval.
Inlet-to-outlet temperature rise.
Calculation method.
Where required, assess:
Calorimeter specification.
Exposed area.
Calibration status.
Burner geometry.
Sampling period.
Thermal-energy distribution.
Correlation with the reference burner.
One satisfactory run does not necessarily demonstrate qualification.
The programme should define:
Number of runs.
Re-light requirements.
Cold-start and hot-start conditions.
Permitted setting changes.
Within-run stability.
Between-run variability.
Between-day variability.
Acceptance of outliers.
The report should distinguish clearly between:
Observed data.
Calculated results.
Acceptance limits.
Deviations.
Engineering judgement.
Customer or authority acceptance.
Scope of burner approval.
Potential causes include:
Incorrect burner modifications.
Wrong nozzle or spray angle.
Deflector-position error.
Extension-tube distortion.
Fuel-pressure instability.
Fuel-flow variation.
Airflow instability.
Soot build-up.
Copper-tube contamination.
Flame non-uniformity.
Burner-to-device positioning error.
Thermocouple ageing.
Potential causes include:
Failed temperature mapping.
Failed heat-transfer measurement.
Instrument calibration delays.
Replacement-part lead times.
Burner maintenance.
Repeated mapping.
Witness availability.
Facility downtime.
Potential causes include:
Burner rework.
Instrument replacement.
Repeat qualification.
Additional test runs.
Fixture changes.
Independent review.
Additional uncertainty assessment.
Potential causes include:
Confusing model identification with qualification.
Applying Report 3A outside its intended scope.
Using acceptance criteria from another standard.
Mixing heat-transfer rate and heat-flux-density terminology.
Failing to reproduce calibration geometry during testing.
Changing burner settings after standardisation.
Inadequate repeatability evidence.
Potential causes include:
Missing burner serial number.
Incomplete modification drawings.
Missing instrument certificates.
Missing fuel records.
Uncontrolled spreadsheets.
Unrecorded setting changes.
Missing raw data.
Ambiguous calculations.
Incomplete deviation records.
Failure to identify the governing standard revision.
Do not describe every pre-test calibration as full burner qualification.
State precisely what the activity demonstrates.
Control the burner as an equipment configuration, including:
Drawings.
Part numbers.
Serial numbers.
Nozzle.
Deflectors.
Cone.
Extension.
Pump.
Motor.
Air settings.
Fuel settings.
Instrumentation.
A burner should be assessed through measured performance, not brand recognition.
Ensure that temperature sensors, water-temperature sensors, flow measurements, pressure measurements and data acquisition are calibrated and suitable for the required range.
Clean and inspect the copper tube before measurement. Carbon deposits can affect heat transfer and undermine repeatability.
Do not record only nominal values. Capture actual fuel pressure, flow, air pressure, water flow, temperatures and geometry.
The uncertainty assessment should consider:
Temperature measurement.
Water flow.
Differential temperature.
Burner positioning.
Timing.
Sampling.
Repeatability.
Environmental effects.
Data-processing calculations.
Retain results over time to identify:
Slow deterioration.
Nozzle wear.
Cone distortion.
Instrument drift.
Increasing variability.
Maintenance effects.
Reverification should be considered after:
Nozzle replacement.
Cone repair or replacement.
Deflector adjustment.
Pump replacement.
Motor replacement.
Air-system change.
Fuel-system change.
Control-software change.
Facility airflow change.
Significant maintenance.
An independent reviewer should challenge:
Applicability.
Acceptance criteria.
Configuration control.
Instrument suitability.
Calculation logic.
Uncertainty.
Deviations.
Release decision.
A controlled burner-assurance package may include:
Burner Qualification Plan.
Burner Qualification Procedure.
Burner Standardisation Procedure.
Burner Configuration Drawing.
Burner Modification Record.
Burner Commissioning Report.
Equipment Register.
Maintenance Instructions.
Maintenance Records.
Calibration Certificates.
Instrumentation List.
Temperature-Mapping Records.
Heat-Transfer Records.
Thermal-Energy Records.
Measurement-Uncertainty Budget.
Raw Data Files.
Data-Processing Verification.
Qualification Report.
Periodic Verification Plan.
Non-Conformance Reports.
Corrective-Action Records.
Change-Control Records.
Test Readiness Review Record.
Requirement Compliance
Every applicable performance and configuration requirement is met.
Flame-Profile Compliance
The required temperature region and distribution are demonstrated.
Heat-Transfer Compliance
The standardisation device demonstrates the required heat-transfer performance.
Repeatability
Repeated runs remain within the defined acceptance limits.
Configuration Integrity
The burner remains in its approved configuration.
Measurement Traceability
The complete measurement chain is documented and traceable.
Verification Closure
All deviations and actions are resolved before the burner is released.
Test Readiness
The burner is approved by the responsible organisation for the defined method, scope and test campaign.
Resonate Testing can support definition of:
Qualification objectives.
Applicable methods.
Burner scope.
Instrumentation requirements.
Acceptance criteria.
Repeatability evidence.
Reporting requirements.
Engineering support can include:
Burner-configuration review.
Flame-mapping methodology.
Heat-transfer measurement.
Test geometry.
Instrument selection.
Measurement uncertainty.
Maintenance and verification controls.
Support may include development of:
Qualification procedures.
Commissioning plans.
Standardisation procedures.
Repeat-run matrices.
Data sheets.
Test readiness checklists.
Deviation processes.
Resonate Testing can support preparation or review of:
Qualification plans.
Calibration records.
Mapping reports.
Heat-transfer calculations.
Uncertainty budgets.
Qualification reports.
Equipment-release records.
Independent technical review can expose weaknesses in burner configuration, instrumentation, calculations, repeatability evidence or scope claims before the burner is used for formal testing.
Support remains subject to:
Technical review.
Equipment suitability.
Safety assessment.
Confirmation of the governing method.
Confirmation of accredited scope where an accreditation claim is required.
Customer or certification-authority acceptance where applicable.
Your Test Facilitator. Not simply a test facility.
What is FAA Report 3A?
FAA Powerplant Engineering Report No. 3A is a standard fire-test apparatus and procedure for flexible hose assemblies. It was revised in March 1978.
What is FAA 3A burner qualification?
It is the process of demonstrating that a defined burner configuration can reproduce the flame characteristics established by Report 3A.
Is burner model alone sufficient?
No. The actual modification state, settings, geometry and measured flame performance must be controlled.
What was the original reference burner?
The reference burner was a modified Lennox OB-32.
Why were replacement burners evaluated?
The modified Lennox OB-32 became commercially unavailable. The FAA therefore characterised its flame and evaluated alternative modified burners.
Why was the Carlin 200 CRD used?
The modified Carlin 200 CRD demonstrated flame characteristics close to the Report 3A reference criteria when configured and operated as documented.
Which other burners appear in Report 3A?
Report 3A also describes modified Stewart-Warner HPR-250 and FR-600 burners.
What flame temperature is required?
Report 3A identifies 2,000°F ±150°F across a horizontal centreline distance of at least seven inches.
What heat-transfer rate is required?
The standardisation flame must deliver at least 4,500 Btu/h to the prescribed copper-tube device. Appendix III also gives an upper controlling value of 4,650 Btu/h.
Is 4,500 Btu/h a heat-flux-density value?
No. It is a total heat-transfer rate measured using the Report 3A copper-tube device.
What water flow is used?
Report 3A specifies 500 lb/h, approximately one US gallon per minute.
Why is the copper tube cleaned?
Surface contamination and soot can change heat transfer and reduce measurement repeatability.
How is heat transfer calculated?
The average inlet-to-outlet water-temperature rise in degrees Fahrenheit is multiplied by the water-flow rate in pounds per hour.
Is one successful calibration enough to qualify a new burner design?
Not necessarily. A qualification programme should demonstrate configuration control, repeatability and all required flame characteristics.
How often should the burner be requalified?
Report 3A does not provide one universal modern requalification interval. The interval should be defined through the laboratory quality system, maintenance history, governing method and customer requirements.
When is reverification required?
Reverification should be considered after changes to the nozzle, cone, deflectors, extension tube, pump, motor, fuel system, airflow system, instrumentation, software or facility environment.
Does ISO/IEC 17025 approve the burner?
No. ISO/IEC 17025 accreditation concerns laboratory competence for defined activities. Burner suitability and method compliance still require objective evidence.
Does FAA Report 3A apply directly to space hardware?
Not automatically. It may be invoked by a space programme, customer specification or project-specific verification requirement.
Does ECSS require FAA Report 3A?
No. ECSS may govern how verification is planned and controlled, but it does not generally mandate the FAA burner method.
Does AS6826 still recognise Report 3A burners?
SAE AS6826 recognises Report 3A burners as capable of producing the required standard flame, provided they satisfy the applicable modern calibration requirements.
Can Report 3A calibration data be used for AS6826?
Not automatically. The AS6826 calibration method, instrumentation, tolerances, recording requirements and post-test validation rules must be satisfied.
FAA Powerplant Engineering Report No. 3A Explained.
AS6826 Powerplant Fire-Test Standard.
ISO 2685 Aircraft Fire Testing.
FAA AC 20-135 Explained.
Aircraft Fireproof vs Fire-Resistant Testing.
Fire-Test Burner Calibration.
Test-Equipment Qualification.
Calibration and Measurement Uncertainty.
Equipment Configuration Control.
Instrumentation Traceability.
Facility Qualification.
Data-Acquisition Verification.
Aerospace Hose Fire Testing.
Aircraft Component Fire Testing.
Firewall Fire-Penetration Testing.
Fluid-System Fire Testing.
Combined Fire and Vibration Testing.
Powerplant Fire-Test Evidence.
Verification Planning.
Verification Matrices.
Test Readiness Reviews.
Test Specifications.
Test Procedures.
Test Reports.
Non-Conformance Management.
Resonate Testing provides technical support for burner characterisation, flame mapping, heat-transfer measurement, qualification planning, measurement uncertainty, test-procedure development and independent evidence review.
Share the burner configuration, governing test method, intended application, existing calibration data and required acceptance criteria for technical review.
Whether you’re looking to contact us for the first time or have another testing requirement, we’d love to hear from you.