Resonate Testing supports your team through qualification, customer acceptance, reliability assessment and environmental compliance using BSG 3G.100-2.3.2, MIL-STD-810 Method 520 and customer-defined combined altitude, temperature and humidity requirements for UK, Ireland and globally-based clients.
Resonate provides combined altitude, temperature and humidity testing for aerospace, defence, transport and advanced engineering programmes. Our BSG 3G-100-2.3.2 and MIL-STD-810 Method 520 testing support helps teams assess equipment against controlled low-pressure, thermal and moisture conditions, with engineer-led planning from requirement review through to reporting.
Combined altitude, temperature and humidity testing exposes equipment to controlled low-pressure, thermal and moisture conditions so teams can assess performance in representative service environments. BSG 3G-100-2.3.2 and MIL-STD-810 Method 520 testing are used to support qualification, compliance and engineering confidence where these environmental stresses need to be considered together.
Altitude simulation: Applies reduced pressure conditions to represent operation or storage at altitude.
Temperature control: Runs agreed hot, cold, ramp and dwell conditions alongside the altitude profile.
Humidity exposure: Assesses moisture-related risks when humidity is part of the specified combined environment.
Functional checks: Allows agreed electrical, telemetry or operating checks before, during or after exposure.
Setup review: Helps confirm chamber fit, instrumentation, cable routing, safety constraints and monitoring needs.
Evidence generation: Produces measurements, observations and reporting to support qualification, compliance or development decisions.
 Humidity
 Temperature
 Altitude
 Vibration
 Shock
Ready to plan your combined altitude, temperature and humidity test campaign? Send your BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 requirement, profile, specification or drawings for engineer review and receive guidance on setup, instrumentation, monitoring and reporting.
Environmental test programmes rarely begin with a perfect specification. Whether you are validating a design, preparing for qualification, planning acceptance testing or checking BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 requirements, an early engineering review can help define a practical route through the combined profile.
Share your equipment description, BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 requirement, altitude level, temperature range, humidity condition, operating mode, instrumentation needs and programme objectives. Resonate Testing can review setup, monitoring and reporting expectations before quotation.
Qualification and acceptance testing support
Aerospace, defence, transport and electronic equipment assessment
Altitude, temperature, humidity and functional monitoring planning
Standards and customer requirement review
Integrated environmental campaign planning
Testing performed to BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 is intended to evaluate how equipment behaves when exposed to combined environmental conditions such as low pressure, temperature, humidity and, where specified, vibration. Typical objectives include assessing functional performance, material response, sealing, condensation risk, electrical behaviour and reliability during the specified environmental exposure.
Test planning is normally based on the specific project and equipment requirements, including altitude level, temperature limits, humidity condition, ramp rates, dwell periods, operating mode, monitoring requirements and reporting expectations. Applicability should be confirmed for the exact equipment, materials and programme requirements before testing begins.
| Standard / Guidance | Primary Focus | Typical Relevance to Testing |
|---|---|---|
| BSG 3G-100-2.3.2 | Combined environmental testing of equipment under simultaneous altitude, temperature and humidity conditions. | Combined altitude, temperature and humidity profile requirements. |
| MIL-STD-810 Method 520 | Environmental engineering procedure for evaluating equipment under combined temperature, humidity, altitude and, where applicable, vibration stresses. | Combined temperature, humidity, vibration and altitude environmental procedure requirements, where specified by the programme. |
| Customer specifications | Project-specific environmental profiles, operating requirements, acceptance criteria and evidence requirements. | Acceptance criteria, operating modes, monitoring requirements and reporting expectations. |
| Product qualification plans | Definition of qualification objectives, test sequencing, sample configuration and acceptance criteria. | Sequencing, sample configuration, pre-conditioning and pass/fail criteria. |
| Safety and operating limits | Safe operation of test articles, facilities and support equipment during environmental exposure. | Power, signal, hazardous materials, stored energy and chamber interface constraints. |
Plan: Review the BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 requirement, acceptance criteria, safety considerations and success measures.
Prepare: Confirm fixtures, sensors, interfaces, telemetry and functional checks.
Mount and instrument: Install the equipment, connect agreed channels and verify the setup before chamber closure.
Condition: Apply the agreed altitude, temperature and humidity transitions under controlled conditions.
Cycle and dwell: Run the agreed combined profile, including ramp rates, plateaus and dwell periods.
Functional checks: Power or operate the hardware at defined points when this is part of the agreed plan.
Review and report: Check achieved conditions, observations, plots, photographs and agreed outputs.
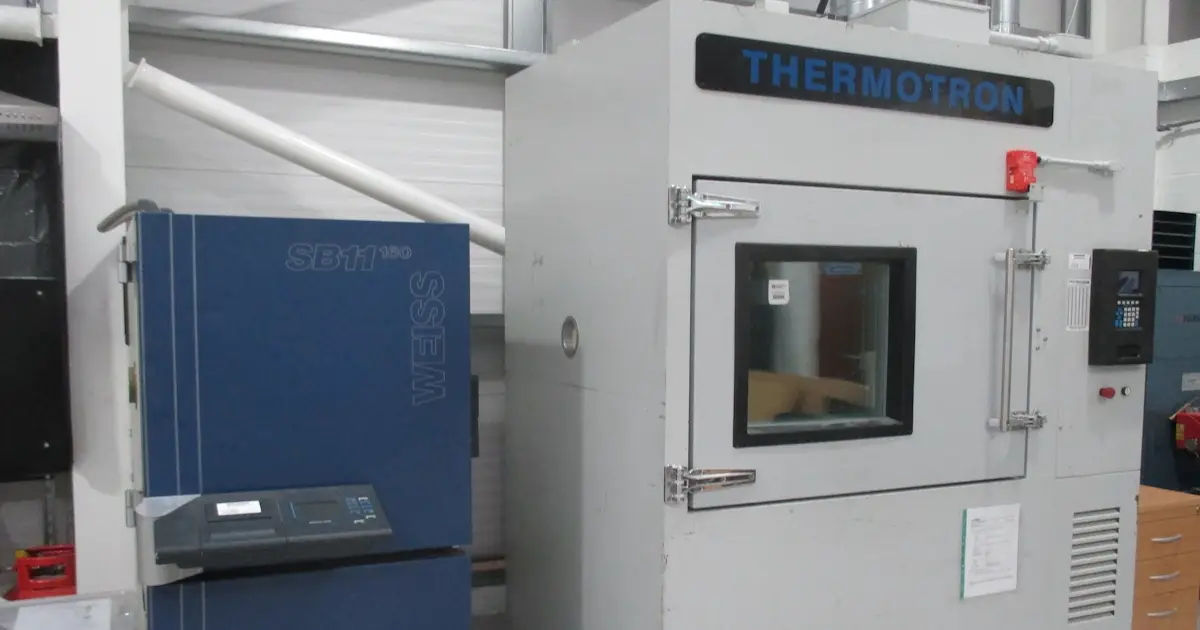
Resonate Testing provides engineer-led combined altitude, temperature and humidity testing for aerospace systems, defence equipment, electronics, batteries and mission-critical assemblies across the UK and Ireland. Programmes can support qualification, customer acceptance, reliability assessment and environmental compliance depending on the agreed specification.
The laboratory supports development, validation and compliance testing for equipment exposed to combined low-pressure, thermal and moisture conditions. Test activity can be planned against BSG 3G-100-2.3.2, recognised standards and customer-defined environmental profiles.
Successful combined environment testing requires more than achieving target chamber conditions. Monitoring and verification may include environmental data, customer telemetry, electrical interfaces, functional checks, pre-test inspection and post-test observations. Altitude level, temperature limits, humidity condition, ramp rates, dwell periods, tolerances and abort criteria should be reviewed before the campaign begins.
For high-value equipment, the fixture and mounting approach are central to the quality of the test. Interface drawings, mass properties, orientation, cable routing and instrumentation access should be reviewed early so the item can be mounted safely and monitored throughout the profile.
Successful combined environment testing depends on more than simply securing chamber time. Early engagement helps identify fixture needs, feedthrough requirements, instrumentation requirements and practical risks before the test campaign starts.
| Specification | Capability |
|---|---|
| Chamber Type | Combined environment chamber |
| Altitude / Reduced Pressure | Simulated altitude up to 100,000 ft |
| Temperature Range (Standard) | -70°C to +130°C |
| Humidity range | 10%–98% RH, depending on temperature |
| Internal Dimensions | 1m x 1 m x 1m - Approximately |
| Usable Internal Volume | Approximately 1m³ |
| Humidity Conditioning | Defined by the agreed combined environment profile |
| Temperature Monitoring | Thermocouple-based monitoring and control |
| Functional Monitoring | Telemetry, electrical interfaces, functional checks, and post-test observations |
| Test Planning Support | Altitude level, temperature set points, humidity condition, ramp rates, dwell periods, thermocouple locations, feedthrough requirements, test sequencing, safety planning, and reporting |
Resonate provides environmental testing that reproduces demanding climatic conditions, including altitude, temperature and humidity. Capabilities include altitude and temperature testing from -70°C to +180°C at simulated altitudes up to 100,000 ft, plus temperature and humidity testing from 10% to 98% RH, depending on temperature.
As an ISO 17025 accredited laboratory with a flexible scope, Resonate can tailor test programmes to the product, operating environment and relevant requirements, supporting standards including RTCA DO-160, MIL-STD-810G/H, IEC/EN 60068 and UN 38.3, where applicable.
With extensive environmental testing capability in one location, Resonate provides a coordinated way to evaluate product and component performance under challenging climatic and reduced-pressure conditions.
Outputs are agreed before the test so the evidence matches the programme need. A typical package may include:
Recorded altitude, temperature, humidity and agreed telemetry data
Plots showing the achieved profile, ramp periods, dwell points and environmental conditions
Observations from setup, test execution and post-test review
Photographic evidence where agreed
Confirmation of functional checks completed during the profile
An agreed test report or data pack aligned to the quotation scope
Hardware dimensions, drawings and keep-out zones
Mass, handling constraints and fixture requirements
Required hot and cold temperature limits
Required altitude or reduced-pressure condition
Humidity condition, ramp rates, plateaus and dwell times
Power, signal, RF, data or thermocouple feedthrough requirements
Telemetry channels and functional checks during test
Battery, pressure vessel, hazardous material or stored-energy safety information
Condensation, sealing, venting or moisture sensitivity concerns
Reporting, photographic evidence and witness requirements
Exposure of equipment to an agreed reduced-pressure condition so performance can be assessed against the specified environmental profile.
A controlled hold at an agreed hot or cold condition, allowing the equipment to stabilise before monitoring, functional checks or the next profile step.
Application of a specified moisture condition during the test profile where condensation, sealing, material response or electrical behaviour needs to be reviewed.
The agreed rate of change between environmental conditions, such as moving from ambient to a hot, cold, humid or reduced-pressure condition.
A steady stage in the environmental profile where altitude, temperature or humidity is held at an agreed level.
Repetition of agreed transitions and dwell periods to assess equipment across multiple environmental exposures.
Testing in which equipment is energised during agreed parts of the profile. Power, signals, telemetry and safety controls should be reviewed before the chamber run.
Agreed inspections or operating checks completed at defined points in the profile to confirm equipment behaviour under the test conditions.
Recording of agreed channels during the test, such as equipment response, environmental data, power, signals or sensor outputs.
A structure that supports or mounts equipment in the chamber. Requirements should be reviewed alongside drawings, mass, handling constraints and keep-out zones.
Interfaces that allow power, signal, RF, data or thermocouple connections to pass into the chamber while the test environment is controlled.
The agreed sensors and data points used to monitor equipment and achieved environmental conditions during the test.
The possibility that moisture forms on or inside equipment during combined temperature and humidity exposure. Sealing, venting and moisture sensitivity should be reviewed before testing.
The means of managing pressure change across equipment, enclosures or cavities during altitude exposure. Venting concerns should be reviewed before the profile is agreed.
Relevant information such as batteries, pressure vessels, hazardous materials, stored energy, operating limits and chamber interface constraints.
Recorded plots showing altitude, temperature, humidity, ramp periods, dwell points and environmental conditions from the test.
A report or data pack summarising agreed outputs, which may include recorded data, observations, plots, photographs and completed functional checks.
Conditions defining whether customer or project representatives need to observe setup, testing, functional checks or review points during the campaign.
Combined altitude, temperature and humidity exposure can reveal risks that may not appear in single-environment tests. Moisture migration, condensation, pressure changes and thermal transitions can affect seals, connectors, displays, electronics, coatings and assemblies.
Risk should be reviewed early if the equipment includes vented enclosures, pressure-sensitive components, adhesives, coatings, batteries, optical surfaces, displays, sensors or live electrical operation. Pre-conditioning, operating checks, recovery periods and inspection points should be confirmed before the test is quoted or committed.
Equipment programmes often need multiple environmental conditions reviewed together. Coordinating altitude, temperature and humidity within one campaign helps reduce handover friction, align documentation and keep the engineering review connected across the full requirement.
For projects that also need corrosion, rain, dust or other environmental testing, review the wider campaign sequence before finalising the test plan.
It exposes equipment to controlled altitude, temperature and humidity conditions so teams can assess performance against a specified environmental profile.
These standards support qualification, compliance or development evidence where combined environmental conditions such as low pressure, temperature, humidity and, where specified, vibration need to be reviewed together.
The duration depends on the agreed profile, including altitude level, temperature range, humidity condition, ramp rates, dwell times, operating checks and reporting requirements.
Yes, if it is part of the agreed plan. Power, signal, telemetry and functional checks need to be reviewed before testing so the correct connections and safety controls are in place.
Provide the BSG 3G-100-2.3.2 or MIL-STD-810 Method 520 requirement, equipment dimensions, mass, altitude level, temperature range, humidity condition, operating mode, monitoring needs and reporting expectations.
Typical outputs may include recorded environmental data, plots of the achieved profile, observations, photographic evidence where agreed, completed functional checks and an agreed report or data pack.
Yes. Early review helps confirm whether the profile, setup, instrumentation, operating mode and evidence requirements are practical before quotation or test commitment.
Book combined altitude, temperature and humidity testing for aerospace, defence, transport, electronics and mission-critical equipment. Use the contact route to share the requirement, profile, drawings or specification for review.
Whether you’re looking to contact us for the first time or have another testing requirement, we’d love to hear from you.